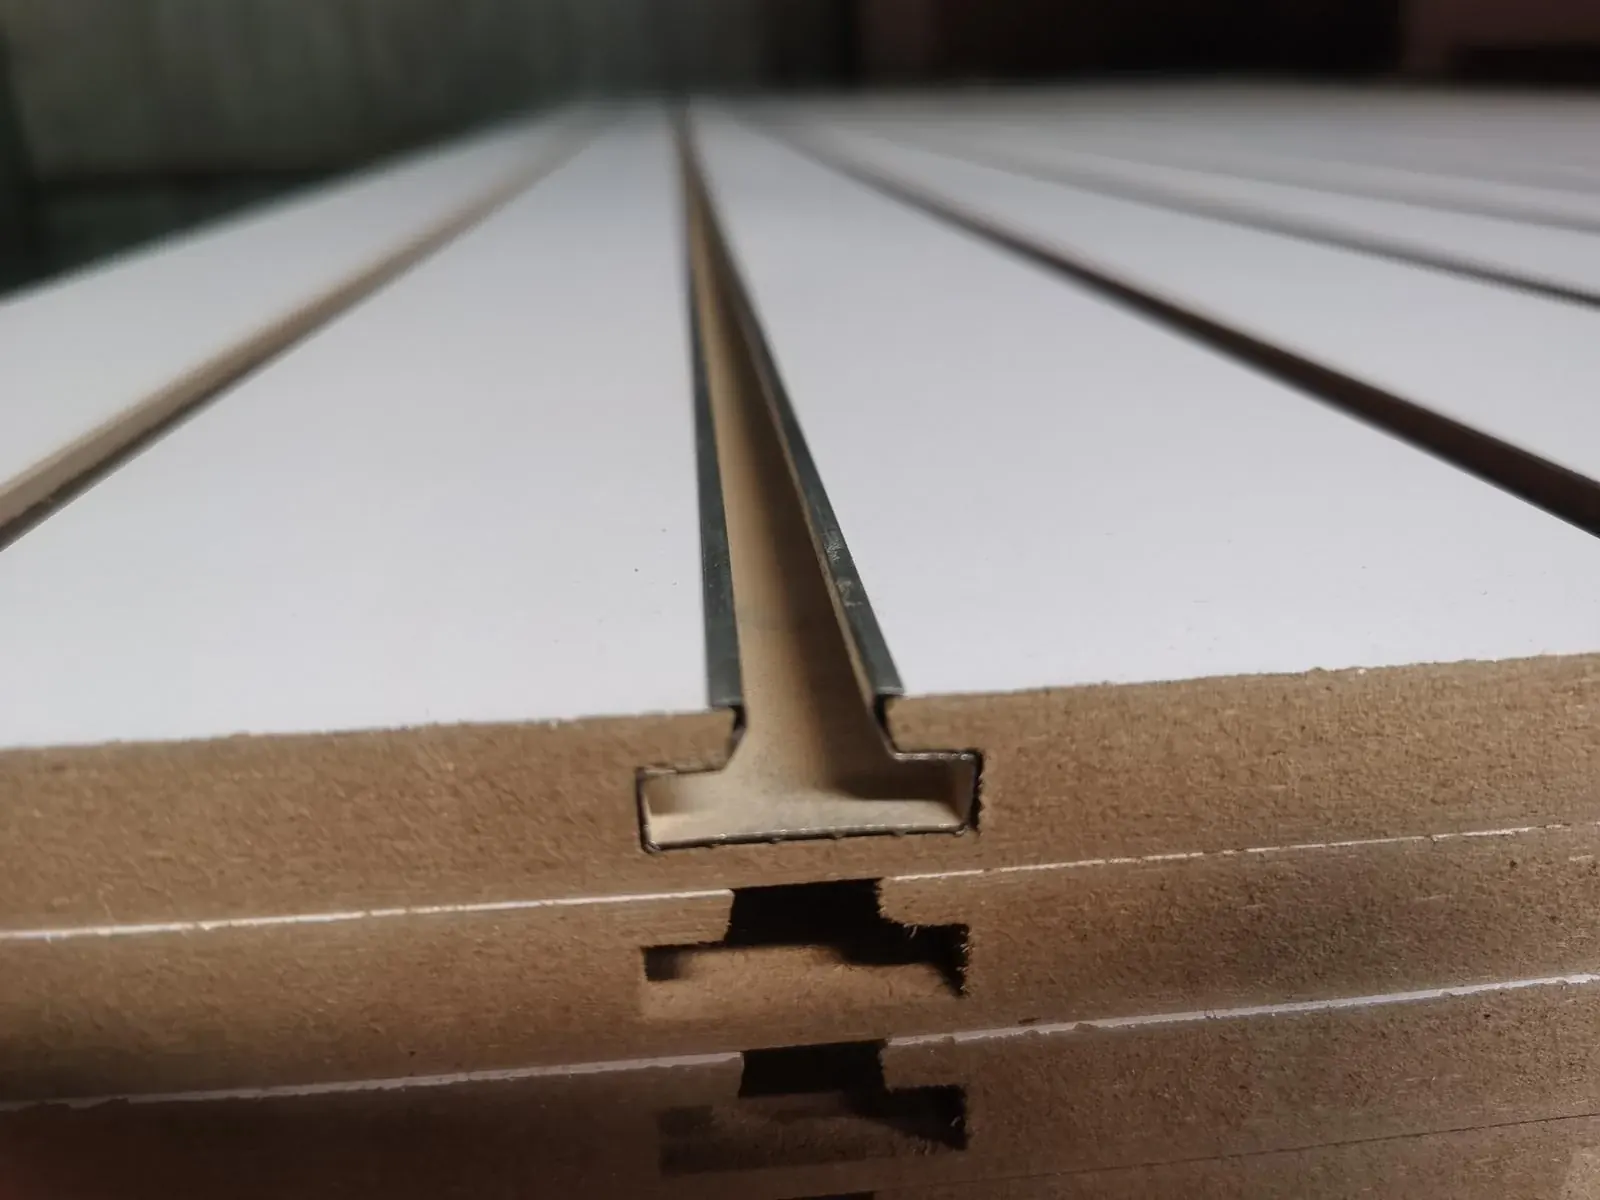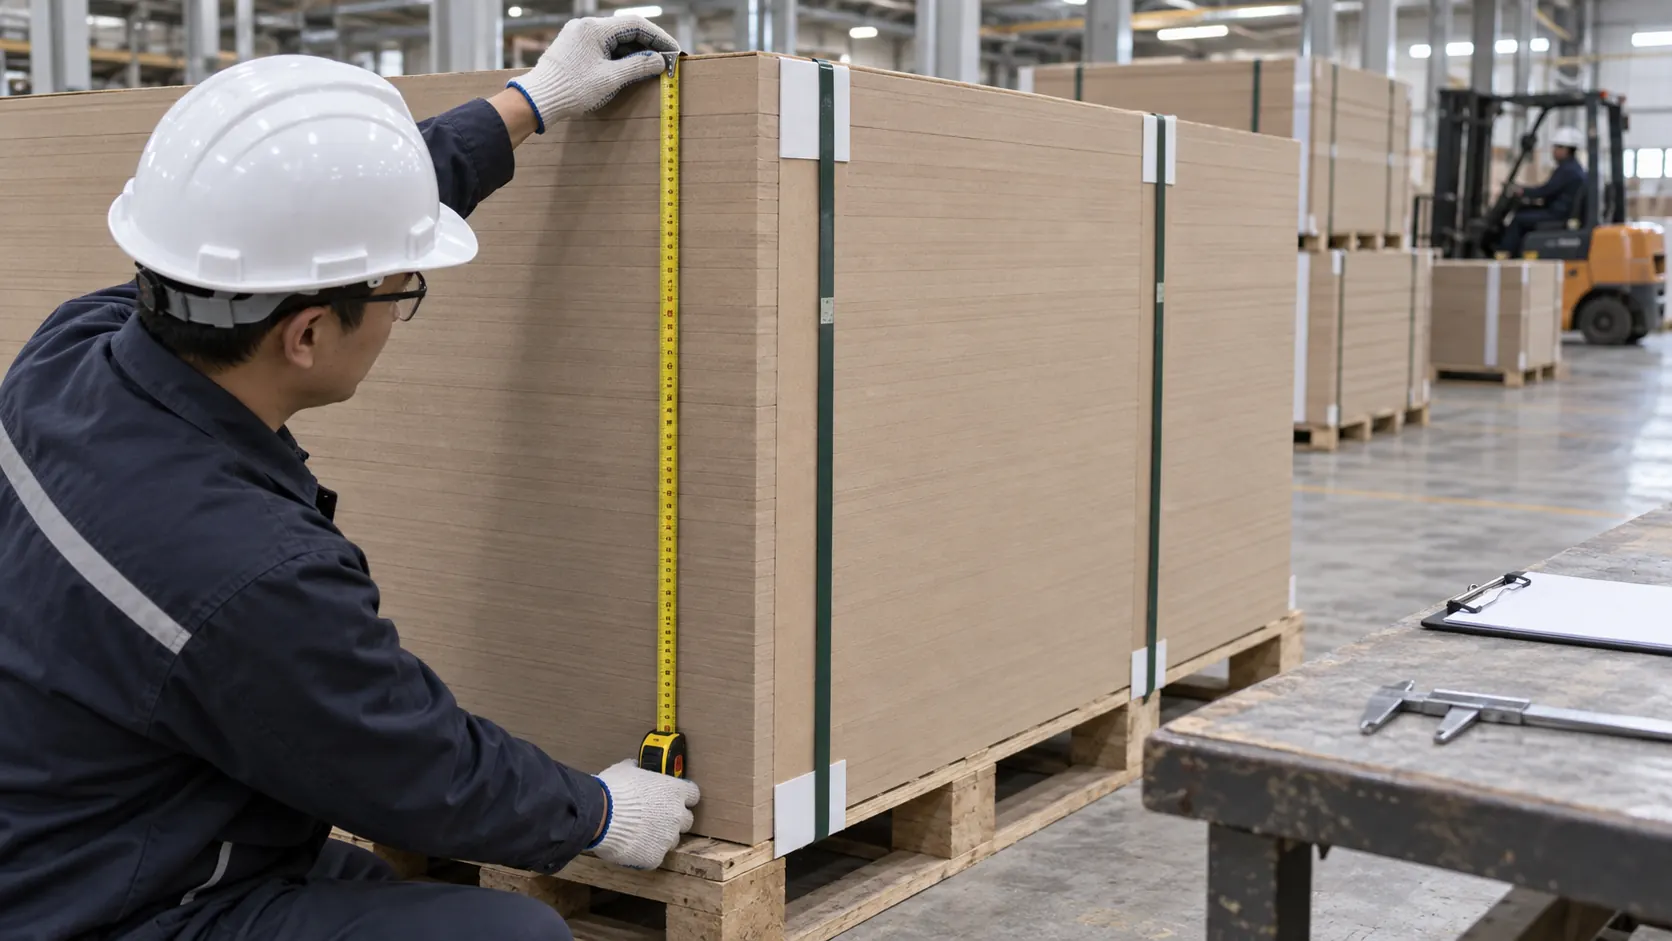
Agree the inspection scope and sampling plan first, then record results clearly enough for a release, rework or reinspection decision.
Arrange the inspection around your production and shipment
An MDF pre-shipment inspection is most useful when it answers the questions your receiving and production teams will face: are these the agreed boards or parts, in the right quantities, with the dimensions, finish, documents and protection the order requires? Plan the visit around accessible goods and a clear written specification. The report then gives purchasing and our factory a practical basis for the next shipment decision.
CUZI MDF manufactures and supplies boards and drawing-defined components from our factory in Shuyang. We support buyer-arranged third-party inspection. Share the lot, selected checks, sampling method, current drawings and samples, required documents and preferred visit date. We coordinate the inspection-ready quantity, access to the goods, document availability and the agreed reporting scope with you and your appointed inspector.
Normal production is 3–10 days after requirements are confirmed. The actual order schedule identifies production readiness, inspection, any agreed corrections, packing and dispatch separately. A visit to inspect accessible faces and machined features may precede pack closure; an exterior-pack review follows completion of the pack. Agree which stages your inspector needs to see, including any loading attendance, so each check has the right access.
Discuss an MDF inspection plan with your specification and proposed scope. We reply within 12 hours. Our quality process explains how we coordinate product checks and documents; this guide helps prepare the record for your particular order.
Keep one current order and sample reference
Start with the version the shipment will repeat. Name the supplied stage: raw board, faced sheet, cut part, routed blank, edge-finished component or completed set. The inspection checks that stage against its own agreed dimensions, construction and appearance. Give each pack and sampled unit an identity that can be found again in the report and packing list.
- Keep the confirmed purchase order, quotation and product specification together with their current revisions.
- Identify the physical appearance or construction samples and the attributes each sample confirms.
- Include current part drawings, cut lists, face/reverse orientation and finish or edge schedules where applicable.
- List the applicable product documents, reports and destination requirements with their required scope.
- Include packing, labels, shipping marks, pack quantities and any matched-set or receiving sequence.
- Agree the lot, sampling method, acceptance criteria, report format and contacts responsible for shipment decisions.
Resolve differing sizes, finish references or revisions before the visit and record the current requirement. Our sample approval guide connects the physical reference with the part drawing and order. The MDF RFQ guide helps put those requirements into a quotation your team can use.
For repeats, identify which sample and drawing remain current, together with the supplied construction. A change in core, face, reverse, edge band, profile or hardware is reflected in the affected inspection checks. This keeps new work and replacement components aligned with the accepted appearance and fit.
Check the product at the stage you are buying
The checklist below is a starting structure. Complete the requirement, method, sample selection and acceptance source for your order. Individual measurements and photographs carry the sampled unit or pack ID. Your report can then show both the observed result and the requirement used to assess it.
| Inspection area | Check and method to agree | Result to retain | Acceptance reference |
|---|---|---|---|
| Product identity | Match product, grade, supplied construction and labels | Order line, product, batch/pack ID and supplied stage | Current specification and order |
| Quantity | Reconcile accessible goods, pack contents and packing list | Sheets/parts per pack, pack count, totals and differences | Confirmed quantities and pack schedule |
| Core and finished thickness | Use the identified instrument and measuring locations | Individual values, units, points and sample IDs | The relevant core or finished-panel requirement |
| Length, width and geometry | Measure at the stated stage with agreed support/datums | Sizes, squareness or flatness results and method | Drawing and agreed tolerances |
| Faces, reverse and edges | Compare the physical reference in agreed light/orientation | Appearance, chips, scratches, contamination and identified photos | Sample and written appearance criteria |
| Decorative construction | Identify face, reverse, finish, direction and edge detail | Decor/veneer reference, construction and supplied condition | Accepted finish and construction schedule |
| Machining and fittings | Measure features from the named datum and review the specified trial | Part/revision, hole or profile dimensions, positions and fit | Current drawing and fitting requirements |
| Moisture or density checks | Use the agreed method for the stated sample condition | Instrument, preparation, readings and calculation basis | Product/order requirement and method |
| Product documents | Match the actual goods and relevant construction to the document | Issuer, reference, dates, pages, method and scope | Destination and purchase requirements |
| Pack protection | Compare completed covers, separators, edges, bearers and straps | Pack dimensions, protection, access and condition photos | Agreed packing specification |
| Traceability and labels | Match pack labels, order lines, quantities and shipping marks | Pack IDs, labels, list revision and set sequence | Label and packing instructions |
| Loading handover | Reconcile packs, mass records, assigned container and seal | Container/seal IDs, counts, loading record and agreed status | Current loading and shipment arrangements |
Use Raw MDF, Thin MDF Board or Thick MDF Board for the identified base board. For a faced order, the actual Melamine MDF, HPL MDF, Veneered MDF, PVC Faced MDF, Acrylic Faced MDF or PET Faced MDF construction establishes which faces, reverse and edges are supplied.
Our Decorative MDF range helps organize finish choices. Cut-to-Size MDF and CNC MDF Processing follow the current part drawings and supplied stage. State which preparation, facing, edge or assembly operations our factory supplies and which your workshop completes. Check the delivered stage against that agreed scope.
Measure core thickness and finished dimensions separately
Our MDF core range is 2–35 mm, with ±0.1 mm core thickness tolerance. The core requirement and a faced or edge-finished component's dimensions have separate entries. Facing, bonding, reverse construction and edge work affect the completed panel. For HPL MDF, the selected nominal HPL face sheet is 0.5–1.2 mm; identify it alongside the core and completed thickness in the order.
Name the instrument, its identification and calibration/verification status, the method, measurement positions, sample condition and units. For thickness, use the agreed thickness instrument and contact arrangement; a tape is useful for larger dimensions and exterior packs. The measuring setup should suit the required resolution and geometry. For a part, identify the front/reverse, datums and support before comparing holes, openings, diagonal checks or flatness.
The following uses assumed measurements to illustrate how a result is compared. The finished-part length criterion of 600.00 ± 0.50 mm is an example project requirement. Its tolerance belongs to this illustration; your actual part tolerances follow the agreed drawing. The 18 mm core row applies our stated core thickness tolerance to an illustrative reading.
| Check | Requirement and permitted interval | Illustrative result and assessment |
|---|---|---|
| Raw MDF core thickness | 18.00 ± 0.10 mm; 17.90–18.10 mm | 18.08 mm; within the stated interval for this reading |
| Finished component length | Assumed 600.00 ± 0.50 mm; 599.50–600.50 mm | 600.80 mm; 0.30 mm above the upper limit |
| The same length after agreed correction | The same assumed 599.50–600.50 mm interval | 600.20 mm; within the interval at recheck |
| Faced-panel thickness | Actual core, face, bond and reverse; agreed completed thickness | Record completed thickness against its own requirement |
| Hole position or profile | Current drawing, entry face, datum and agreed tolerance | Record the individual feature coordinate, depth and result |
| Squareness or flatness | Agreed geometry, support, method and permissible result | Record the measuring arrangement and values assessed |
A reading within its interval answers the sampled dimensional check. The full inspection decision also uses the agreed sample results, quantities, appearance, documents and packing checks. Keep nominal, measured and calculated values identified. The European Panel Federation's property guide explains different assessments of MDF properties; use the applicable method and product requirement for each check.
For moisture content, agree the device or laboratory method, sample condition and measuring positions. Our moisture, storage and conditioning guide helps organize that record. For a density calculation, retain specimen mass and actual measured dimensions in the stated units; our density guide develops that calculation. Product grade and performance remain connected to their own relevant reports.
Agree the lot and sampling plan before the visit
The inspection plan defines the lot, sample selection, equipment or method, sample size and acceptance criteria before inspection begins. Use tolerances and sample counts supported by the approved order basis. Identify how the inspector will access the selected units across the presented packs and which checks require opening or handling.
The appropriate sample count follows the order size, risk, product construction, process, destination requirement and consequence of a missed defect. A sample represents the selected units; the lot decision follows the agreed acceptance procedure. An appearance check assessed as conforming/nonconforming and a dimensional reading retained as a measured value each need the correct recording and decision method.
| Sampling-plan field | Information to agree | What the report should show |
|---|---|---|
| Lot identity | Order lines, grade/finish, batch or production group and quantity | The actual presented lot and inspection-ready quantity |
| Sample selection | How units and pack positions are selected and accessed | Selected pack/unit IDs and the selection method |
| Check scope | Dimensions, appearance, machining, pack or document checks | Checks completed and any access limitation |
| Sample quantities | Quantity assessed for each check and any destructive test | Actual inspected numbers and stated unit basis |
| Acceptance procedure | Required standard/procedure, edition and agreed criteria | The applicable decision rule and recorded result |
| Defect classification | Agreed definitions and examples for relevant categories | Identified observations classified by the agreed definitions |
| Follow-up | Actions for differences, repeated checks and decision contacts | Affected scope, actions, recheck and written outcome |
Where your contract selects acceptance sampling by attributes, identify the procedure and edition, inspection level, AQLs for the agreed categories, applicable scheme and acceptance/rejection rules. ISO's ISO 2859-1:2026 overview identifies its scope as AQL-indexed acceptance sampling by attributes for lot-by-lot inspection. The actual inspection uses the agreed procedure's tables and rules. Record the choices before applying them to the presented lot.
A product-page tolerance and an AQL serve different purposes. The tolerance defines the permitted result for a characteristic; the sampling procedure establishes how selected observations support the lot decision. Retain the individual readings and affected unit IDs so a later recheck can address the same requirement and scope.
Record differences and close the agreed actions
An inspection report is useful when your team can understand exactly what was observed and what happened next. Record the requirement, actual result, unit/pack identity, affected quantity or scope and supporting photograph. Identify the responsible contact and the action agreed with your purchasing team. Keep the original observation and the follow-up together.
The table below continues the illustrative finished-length example. EX-P03 is a pack ID and EX-S02 a sampled component ID. They describe an example record, separate from an actual CUZI inspection. The actual affected quantity is established by the agreed review of the identified goods.
| Record step | Illustrative entry | Next action |
|---|---|---|
| Requirement | Component EX-S02, drawing EX-D/r4; 600.00 ± 0.50 mm | Retain the current drawing and measuring reference |
| Original observation | Pack EX-P03; measured length 600.80 mm | Identify the unit and establish affected scope |
| Initial status | Hold for the identified dimensional issue | Agree correction or another written disposition |
| Correction | The agreed dimensional correction is completed | Retain the action and actual affected quantities |
| Recheck | The same requirement measures 600.20 mm | Record method, unit, date and the recheck result |
| Shipment decision | Authorized written outcome after required checks are complete | Link the resolved issue and remaining inspection results |
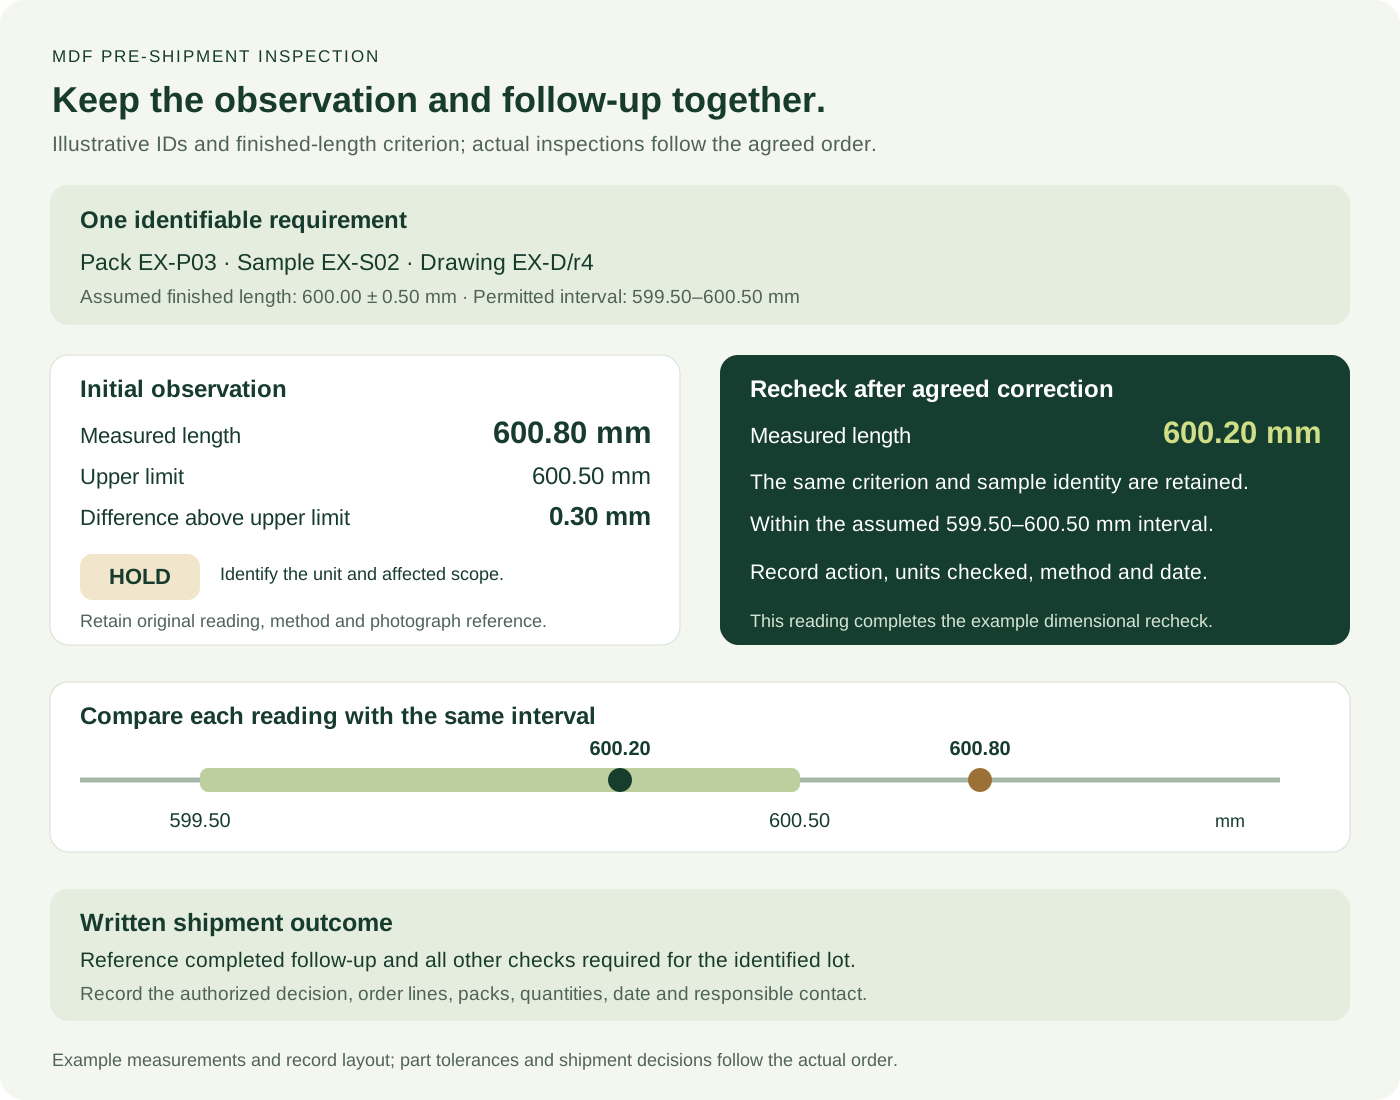
The diagram separates a measured characteristic from the complete shipment decision. In the example, 600.80 mm exceeds the assumed upper limit of 600.50 mm by 0.30 mm. The 600.20 mm recheck falls within the assumed interval. The written outcome then references the completed follow-up and all other checks required for the lot.
Use clear statuses such as pass, hold, correction and recheck, or an agreed written deviation for the identified scope. Goods placed on hold receive their agreed corrective action, reinspection or authorized written disposition before shipment. A partial release identifies exactly which order lines, packs and quantities are included, alongside the remaining balance.
Agree who can decide a correction, replacement, written deviation or shipment release. The inspector records the observed results and the conclusion within their agreed scope; the purchase agreement establishes the responsible decision contacts. Keep any deviation attached to its specific requirement, goods and order revision so a repeat order uses the intended specification.
Match product documents to the inspected goods
Use laboratory test reports and a product-document review for material properties, formaldehyde emissions, mechanical performance, fire performance and moisture-related classification. A visual or dimensional inspection records the features assessed under its stated method. Product-performance questions use the relevant method, actual construction and document scope.
| Document question | What to match | Information to retain |
|---|---|---|
| Which material is covered? | Manufacturer/product, grade, thickness and sample or batch reference | Actual supplied product and document identity |
| Which construction is covered? | Core, face, reverse, bond and finished condition where relevant | Complete offered construction and scope |
| What was assessed? | Property, standard/method, conditions and result | Relevant pages, units and applicable requirement |
| When and by whom? | Issuing body, document reference, date and applicable status | Traceable document and relevant current scope |
| What does the destination require? | Named US, EU, UK or project purchasing requirement | The requested document set for the actual goods |
| What remains to complete? | Missing information, further test or agreed follow-up | Responsible contact, timing and written outcome |
List the checks completed, any outstanding test reports and the points to resolve before shipment. Keep these with the inspection report and order details. Our certificate and test-report guide helps match those records with the product.
For US purchasing, use our TSCA Title VI MDF document checklist for the requested product scope. For EU orders, our MDF import document guide organizes the applicable purchasing documents. Fire-performance requests identify the actual board or assembly and required classification; the fire-rated document guide explains the comparison.
Third-party inspection and laboratory testing can form different parts of the order review. Agree each scope, sample preparation, access, reporting, timing and any associated service arrangements. Request the documents for your MDF order with the product, construction and destination requirements.
Check completed packs and the loading handover
A good panel inspection and a good pack inspection work together. Complete the accessible product checks at the agreed stage, then confirm the exterior pack and protection. The packing list connects each completed pack with the sheets, components or matched sets inside it.
| Handover check | Information to record | Order reference |
|---|---|---|
| Face and edge protection | Covers, separators, edge/corner guards and actual condition | Finish and packing requirements |
| Support and handling | Bearers, contact positions, fork access and agreed equipment | Pack and handling arrangement |
| Pack dimensions and mass | Exterior dimensions, counts and measured/calculated mass basis | Current packing schedule |
| Labels and contents | Pack IDs, order lines, counts, drawing/finish references and sequence | Packing list and label instructions |
| Assigned container and loading | Container identity/condition, relevant equipment data, pack positions and photos | Booking and loading arrangement |
| Seal and shipment records | Final pack count, container/seal IDs, documents and agreed outcome | Final handover and transport records |
- Complete the agreed checks while the selected goods and surfaces remain accessible.
- Compare pack protection, support, dimensions, mass and labels with the current packing instructions.
- Reconcile sheets or components per pack, total packs and order-line quantities on the final packing list.
- Confirm loading arrangement and mass records against the assigned equipment and applicable shipment conditions.
- Record identified loading photographs, container and seal details, with the agreed shipment outcome.
- Give your receiving team the packing list, opening sequence and contact details for any arrival discrepancy.
Our MDF packaging guide explains face, edge and pack protection. The container loading guide separates board volume, exterior pack volume, cargo mass and container-total verification. The recorded 18 mm E1 loading case demonstrates one shipment's quantities and masses. Your inspection record identifies the actual order and container being checked.
At receiving, reconcile the shipment identity, labels, quantities and condition before the next processing or assembly step. Photograph identified packs and record any discrepancy with its pack ID. Share the finding with our team so the order, inspection and arrival records can be reviewed together. See our packaging and shipping process for the overall handover.
Send the requirements for your inspection visit
The earlier we receive the scope, the easier it is to coordinate access, references and timing. Send the current checklist alongside the product or component specification. We can then confirm which checks need raw boards, open components, finished packs, documents or attendance during loading.
- Product, grade, thickness or completed construction, dimensions and quantities by order line.
- Component drawings, cut list, face/reverse orientation, edge details and current revision references.
- Physical samples, finish references, viewing conditions and accepted appearance criteria.
- Lot definition, sampling procedure, equipment/method, sample counts and dimensional or other acceptance requirements.
- Inspector details, proposed visit date, required access and any laboratory or destructive-test scope.
- Documents, applicable destination requirements, reporting format and photograph references.
- Pack, label, loading and destination unloading instructions, including mixed or matched sets.
- Contacts for decisions, agreed follow-up, shipment dates and any partial-release requirements.
Coordinate a pre-shipment inspection visit with the scope and preferred date. We support third-party inspection and reply within 12 hours. Normal orders start from 1 × 20'GP per specification, with 3–10 day normal production after requirements are confirmed. Actual inspection, correction, cargo-ready and dispatch dates are coordinated for the order.
Our formal quotation includes the specification, quantity, price and currency, packing, trade term and named place, lead time, payment conditions and validity. FOB, T/T or L/C, and shipment through Lianyungang or Qingdao are available. Send your RFQ and inspection requirements or contact sales@cuzimdf.com.
Free product samples are available across our range and usually in stock. You pay the courier charge, which can be credited against the formal order amount. We confirm sample preparation, dispatch and estimated courier transit for your request. Request an MDF product sample to establish the material or finish reference before the order's inspection checks are finalized.
Questions buyers ask
Can I arrange third-party inspection at CUZI MDF?
Yes. We support buyer-arranged third-party inspection at our factory. Agree the lot, timing, access, sampling, checks, drawings/samples, documents and reporting scope before the visit. Include loading attendance if it is part of your requested service.
When should the inspection take place?
Arrange it when the agreed lot or quantity is ready and accessible for the selected checks. Faces, edges and machined features may need open goods; protection checks need completed packs. Coordinate inspection, any corrections, final packing and dispatch as separate milestones.
Which MDF checks should the report include?
Identify product and quantity, then the dimensions, appearance, finish, machining, documents, labels, packaging and loading checks relevant to the supplied stage. Every result carries the requirement, method, sampled unit or pack ID and the recorded decision.
Which dimensional tolerance should we use?
Use the agreed specification and current drawing. Our core thickness tolerance is ±0.1 mm; finished-panel thickness, cut sizes and machining features have their own agreed requirements. Identify the actual supplied stage and measuring method beside the result.
How many sheets or parts should the inspector sample?
Agree the lot and sampling procedure for the order and each check. Where an attribute-sampling standard is selected, record its edition, level, categories, AQLs and applicable decision rules. Record the actual units inspected and their selection. The report uses the agreed plan to assess the lot.
Does a conforming dimensional sample establish fire or emission performance?
The sample result addresses the measured characteristic. Fire, emission, mechanical or moisture-grade questions use applicable reports and document scope for the actual supplied product/construction. Record those reviews alongside the visual and dimensional checks.
How do we check colours and decorative faces?
Use the identified physical reference, agreed light, orientation and supplied condition. Compare the relevant face, reverse, pattern, texture, gloss and edges. For veneer or matched panels, retain set identity and sequence. Record accepted variation in terms your team and our factory can apply.
What happens when the inspector records a difference?
Identify the affected goods and scope, record the requirement and observed result, then agree correction, replacement or another written disposition with the responsible contacts. Retain the original finding and the recheck. The shipment decision references the resolved issue and other required results.
Can part of an order ship after inspection?
A partial shipment follows an agreed written scope. Identify the released order lines, packs, quantities and the remaining balance, alongside their inspection and packing records. Confirm the effect on booking, documents and receiving sequence for that shipment.
How do inspection results connect to receiving?
Give your receiving team the final packing list, labels, relevant report and opening instructions. Reconcile shipment identity, pack counts and condition at arrival. Record identified photographs and discrepancies before the next production step so our team can review them with the order records.