
Define both supplied faces
Identify Face A and Face B, acceptable marks and any additional sanding. Abrasive grade and measured surface roughness are different specifications.
Professional MDF Manufacturer & Supplier
A smooth start for the finish your furniture deserves. We manufacture Sanded MDF in Shuyang, China, with smooth faces and custom preparation for pressing, veneering, laminating or painting.
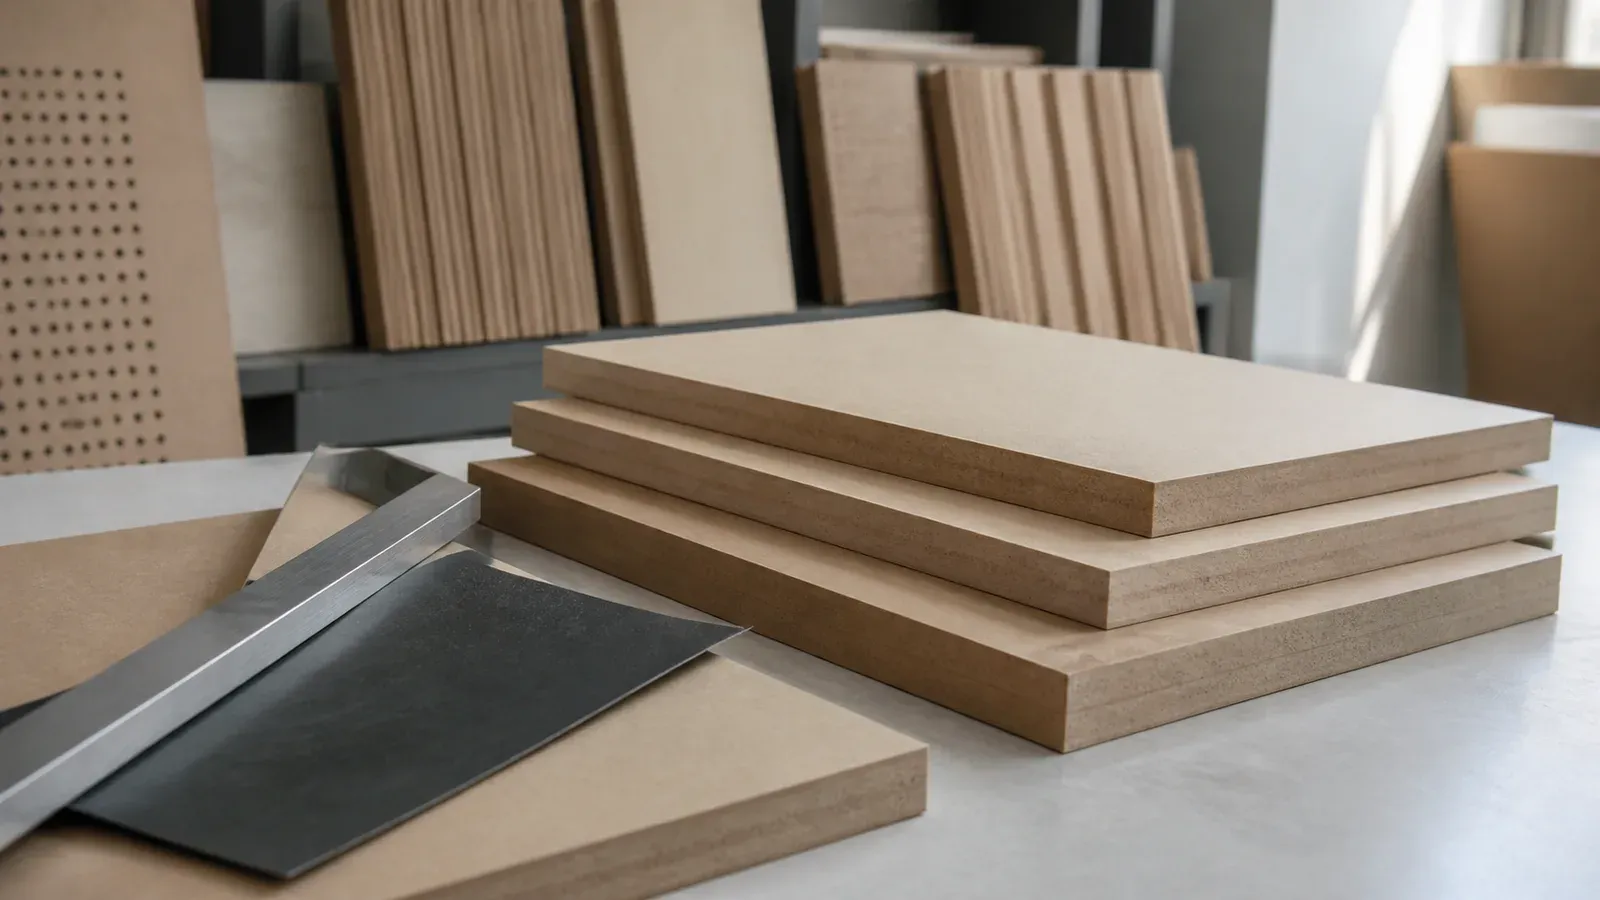
Technical specification
Sanded MDF has factory-sanded faces for painting, veneering, lamination and other finishing. Specify the face condition and any additional preparation needed for your workshop process.
Finish and processing
Identify Face A and Face B, acceptable marks and any additional sanding. Abrasive grade and measured surface roughness are different specifications.
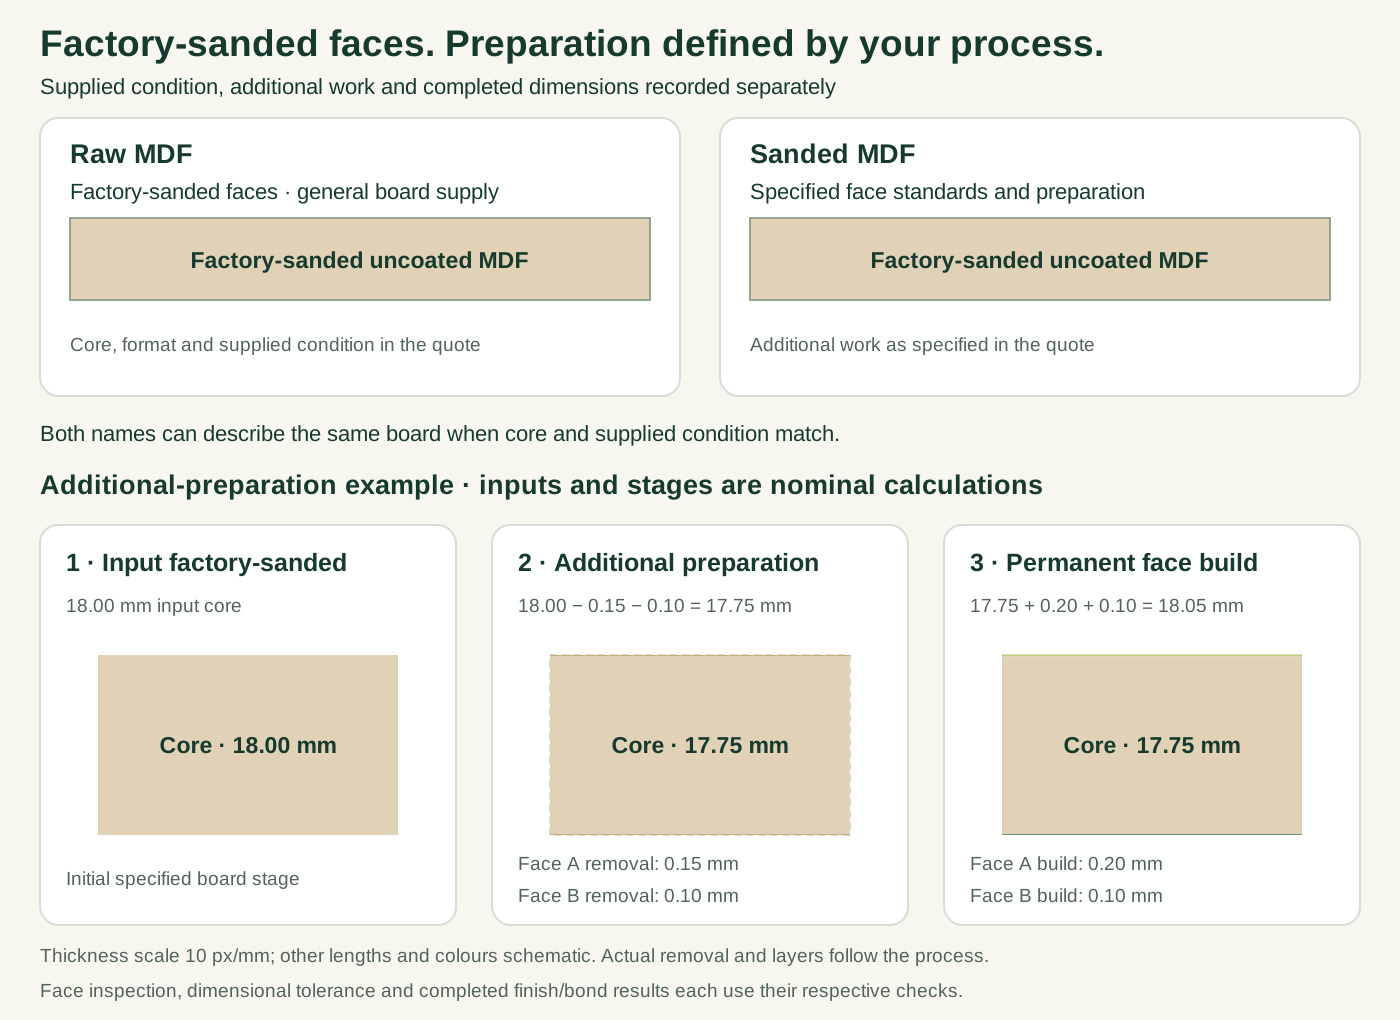
Additional sanding removes material; veneer, adhesive and coatings add it. Record the input board, prepared core and completed component thickness separately.
Check the chosen coating or adhesive on the actual face and cut edge. Keep surfaces dry, clean and protected through storage and processing.
Selection guide
For the core behind the sanded surface, read what MDF is made of and how it is manufactured. Then choose the surface preparation for your next coating or laminating operation.
Your next coating or pressing operation begins with the surface it receives. CUZI MDF manufactures 2–35 mm Sanded MDF in Shuyang, Jiangsu, China, with the selected core, supplied face condition and protected delivery recorded together. Tell us whether the board is going to paint, veneer, melamine pressing, another laminate or component machining. We can organize the material and agreed preparation around that next stage.
Our Raw MDF also has factory-sanded faces. Both names can describe the same board. Choose Sanded MDF when face smoothness and preparation are especially important for your next process. Tell us how you will use the board, and we will include any extra preparation in the quote.
| What you are purchasing | Information that defines the supplied stage | Where the product detail helps |
|---|---|---|
| Raw MDF | Selected core, thickness, format and factory-sanded uncoated faces | General board supply and subsequent processing |
| Sanded MDF | Selected core plus agreed face criteria, preparation and dimensional checks | Surface-condition requests for your finishing or pressing line |
| Paint Grade MDF | Substrate, faces, cut/profiled edges and the complete coating trial | Choosing the material and preparation for your painted component |
| Faced or finished component | Actual permanent surface, reverse, edges and completed dimensions | Buying the stated decorative or finished supply stage |
Use the Raw MDF page for general MDF format and core requests, and Paint Grade MDF for the complete painted-part selection. Tell us whether you need an uncoated board, prepared part or finished component so we can quote the work your factory needs.
The photos show the board faces, edges and surface checks. Try a physical sample to check the face and its response to your finishing process. If you need a particular sanding grade or measured surface roughness, send the requirement with your inquiry.
Keep the existing board specification if it already fits your line, adding the face or preparation criteria that make the next batch easier to receive and use. When a different core grade, sanding operation or supplied finish is required, describe the changed item and its sample trial. The comparison between offers then follows the same core, preparation and delivered condition.
Identify Face A and the reverse Face B, including which side is visible and which will be coated or bonded. Agree whether both sides share the same face standard. A visible furniture front, a balancing reverse and a concealed component surface can have different specified checks. Part labels, drawing orientation and any finish reference keep the faces connected through cutting and preparation.
State the required sanding sequence or abrasive grade where your process specifies it, with the agreed supplied stage. Abrasive grading identifies a process input. The actual face condition also follows the equipment, abrasive condition, material, feed and preparation. Where surface roughness is required, identify the parameter, measurement method, instrument and sampling conditions, together with the allowed value for the intended process.
| Face criterion | What the request specifies | How the reference is recorded |
|---|---|---|
| Face A / Face B | Visible/contact face and standard for each side | Face photographs, sample ID and supplied stage |
| Sanding process | Required sequence or grade and any additional preparation | Agreed process specification and representative sample |
| Marks and defects | Acceptable sanding marks, scratches, dents and edge condition | Reference sample/photos with stated viewing conditions |
| Cleanliness | Dust/contact cleanliness for the next coating or bond | Agreed cleaning, handling and packaging checks |
| Measured surface or geometry | Required roughness, thickness or flatness criterion and method | Actual measurements, positions, conditions and acceptance values |
For an appearance check, record lighting, viewing angle, distance and which surface or region is inspected. For a measurable parameter, specify the actual method and sampling arrangement. A roughness parameter such as Ra or Rz has its stated measurement meaning; an abrasive grade and a visual sample provide their own different information. We agree the available face/process specification and required checks with your order.
Separate local face marks from whole-panel shape. Bow, twist, thickness variation and surface roughness are different conditions, each checked with its relevant method and support. Identify flatness measurement support and reference span, board conditioning and positions on the sheet where needed. That makes inspection results easier for both teams to compare after storage or transport.
Include sawn edges, routed profiles, recesses and hole exits when they affect the finish. Those surfaces are created by their own operations and receive the preparation your component needs. The MDF edge preparation guide connects cut edges with sealing and painting, while CNC processing records the geometry and supplied machining stage for parts.
The listed Sanded MDF thickness range is 2–35 mm, with nominal board-thickness tolerance ±0.1 mm under the agreed measuring and acceptance method. Six reference formats are 1220 × 2440 mm, 2100 × 2800 mm, 1830 × 3660 mm, 1830 × 2440 mm, 2440 × 3660 mm and 1830 × 4200 mm. Choose the input format with your nesting plan, handling and ordered quantity.
Measure the board at its stated supply stage. Additional calibration or sanding removes material, while permanent face/reverse layers add their thickness. A component drawing therefore identifies the dimension reference before preparation, after any extra work and at the final supplied or assembled stage. Cutting, hole or groove tolerances and finished faced-panel thickness each have their own agreement.
As a nominal calculation example, an 18.00 mm input board receives an additional 0.15 mm removal from Face A and 0.10 mm from Face B. The resulting core is 18.00 − 0.15 − 0.10 = 17.75 mm. Adding an illustrative 0.20 mm Face A build and 0.10 mm reverse build gives 17.75 + 0.20 + 0.10 = 18.05 mm. These are selected geometry inputs; actual removal, layer construction and tolerances are established for the operation and component.
| Example stage | Nominal calculation | Dimension record for the actual order |
|---|---|---|
| Input factory-sanded board | 18.00 mm | Board thickness at its specified supplied stage |
| Additional preparation | 18.00 − 0.15 − 0.10 = 17.75 mm | Measured prepared core and removal/process record |
| Permanent face and reverse build | 17.75 + 0.20 + 0.10 = 18.05 mm | Actual layers, bonding where used and finished thickness |
| Assembly or further machining | Fit checked against the completed dimension | Groove/hardware reference and separately agreed component tolerance |
The input board's tolerance describes that material stage. A specified prepared thickness or completed panel size has its own nominal value, tolerance and measuring basis. The example's 17.75 mm prepared core and 18.05 mm completed sample are calculated stages of an illustrative component. They demonstrate why the quote records the stage being measured and supplied.
Where further sanding is requested, agree the intended result, each face's work and the related dimensional checks. Material removed can affect profiles, edges, fit and the region of the core exposed to finishing. Record the actual prepared state with the process trial. For a laminate or veneer construction, identify permanent face/reverse layers and bonding thickness as relevant to the completed measurement.
Our Cut-to-Size MDF service connects a component list to its finished dimensions and packing. A cut part, a sanded uncoated part and a complete edged/faced part are quoted at their respective stages. Keep the drawing revision, datums, face direction and quantity with those dimensional requirements, especially for repeat fronts or adjoining panels.
Try a sample with the board, finish and machining you plan to use. Include a flat face, cut edge and any routed detail, then run it through your preparation and finishing process. Keep it as the reference for your order.
| Your next process | What the trial uses | Result and information retained |
|---|---|---|
| Painting or lacquer | Actual sanding/cleaning, edge preparation, sealer/primer and topcoat | Appearance, profile detail, relevant coating checks and process reference |
| Veneer or bonded laminate | Actual face/reverse materials, adhesive and pressing/cure conditions | Bond, balance, completed dimensions and physical surface sample |
| Melamine pressing | Selected core, paper/resin system, preparation and press conditions | Surface result, relevant bond/property checks and identified construction |
| Machining before finish | Actual cutting/routing, local features and subsequent preparation | Geometry, edge/profile quality and the completed finish trial |
For paint, identify the coating system and the steps between bare material and the completed surface. Broad faces, cut edges and routed details can call for different preparation within that system. Inspect the finished part at the agreed lighting and stage, including corners, recesses and new cuts. The MDF painting guide develops the substrate and complete coating request.
The European Panel Federation's edge-sanding guidance relates preparation methods to profile detail and the subsequent finish. Use a suitable operation for the actual shape, retaining the dimensions and detail that matter to the part. The selected abrasive, machine conditions and final preparation are established by the representative trial, with the actual result recorded.
For veneer or a bonded laminate, specify face material, adhesive, pressing/cure, reverse/balancing construction, edge treatment and final dimensions. Inspect the bond and finished panel using the agreed method. The EPF veneer guidance discusses the substrate and veneering process. Our Veneered MDF and Laminated MDF pages identify their complete supplied constructions.
Melamine pressing uses its chosen core and paper/resin system with the actual pressing conditions. A completed melamine face is described by that construction and its sample. Melamine MDF covers that finished surface request. Coating appearance, adhesion, wear, stain or moisture requirements each use the relevant finish/system checks and product scope alongside the supplied Sanded MDF record.
A repeatable preparation standard benefits from consistent handling. Keep panels supported flat in dry covered storage and use clean contact materials between sensitive faces. Protect edges, corners and prepared features during lifting and movement. Conditioning and moisture content are agreed for the actual workshop process; the selected core grade and complete finish follow the room and intended service.
Standard Sanded MDF is an interior preparation supply. Humid indoor uses call for the selected MR MDF or HMR MDF core and relevant moisture data, with faces, edges and joints included in the finished component. A fire requirement follows the actual FR product or construction documents. Sanding condition describes surface preparation within the chosen material and system.
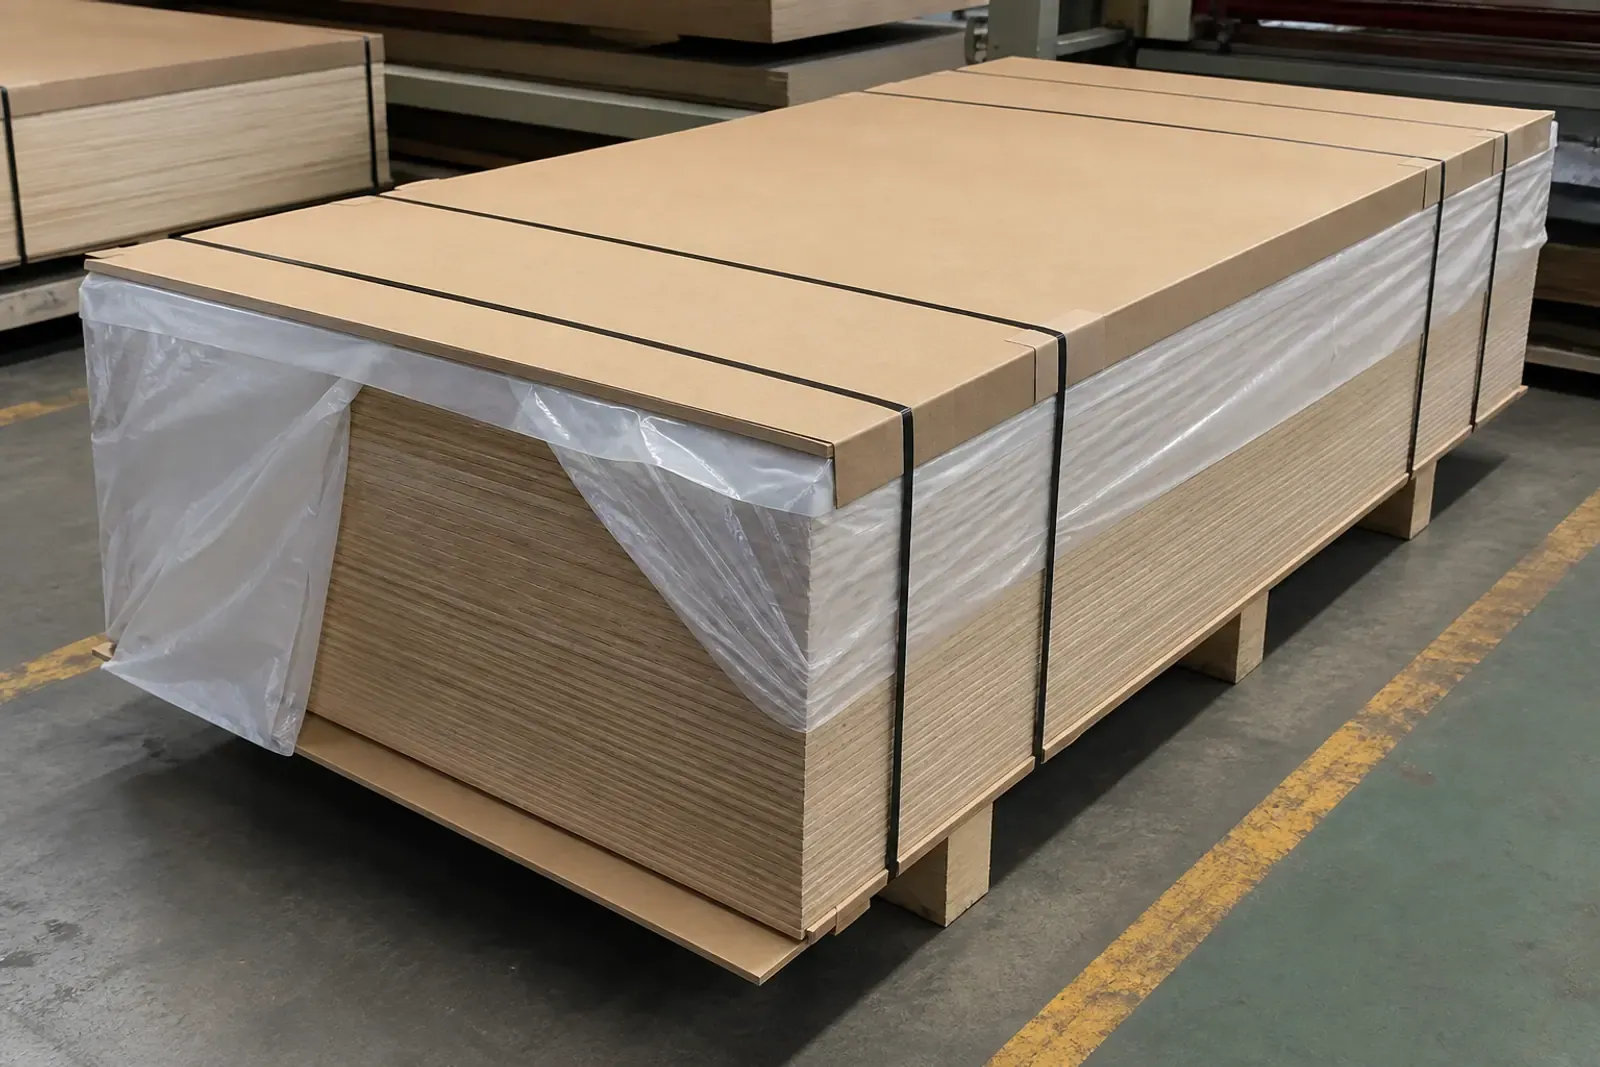
Match clean separators, cover boards, supports, wrapping and controlled strapping with sheet size, face sensitivity and receiving equipment. Prepared surfaces and routed features receive suitable protection. Pack labels can identify core/thickness, supplied preparation, Face A/B where needed, part or batch ID, quantity and drawing revision. The receiving team can then check the face condition against the correct sample and order.
For bare-sheet handling, calculate volume in metres and multiply by the stated density in kg/m³. A nominal 1220 × 2440 × 18 mm input sheet has volume 0.0535824 m³. At the listed 12–18 mm density inputs 680–750 kg/m³, its calculated bare mass is 36.44–40.19 kg. Measured product dimensions, density and moisture condition establish the corresponding actual mass. Additional removal or permanent layers each affect their respective component mass.
A nominal 20-sheet stack at those bare-sheet inputs calculates to 728.72–803.74 kg before packing. Twenty is a calculation example, with actual pack counts agreed for shipment. Gross mass includes the actual covers, pallet/bearers, wrapping, straps and other packing. Loading quantity combines actual dimensions, density, pack construction and the shipping plan. Keep bare-sheet estimates, completed parts and gross pack weights identified separately.
Retain the core/product reference, sample ID, thickness/density, input format, supplied face standards and any additional work. Add inspection methods, measurement positions and conditions, acceptable mark references, Face A/B criteria and the actual coating or pressing trial result. When your process changes, record the revised materials or preparation and the representative result with the current specification.
Tell us the emission requirements for your destination and ask for the relevant board reports. Before dispatch, check dimensions, faces, edges, quantity and packing against your order and sample. Third-party inspection is welcome.
All product samples can be requested free of charge and are generally in stock. The buyer pays the courier cost, which can be credited against a formal order. Send the thickness, face criteria, next process and delivery address; we confirm availability, dispatch, courier cost and estimated transit time. We will give you a preparation date for a custom component. We reply to inquiries within 12 hours.
FOB China price: US$175–258/m³ for Sanded MDF. Compare the same core grade, density, thickness, format, face requirements, supplied preparation and quantities. The quote identifies additional sanding, machining, priming, facing or other requested work by its actual scope. Normal MOQ is 1 × 20'GP per specification. Normal lead time is 3–10 days after specification and commercial confirmation, with additional operations following the written schedule.
MDF board production capacity is 500 m³ per day across the factory. Additional preparation or component output follows the specified operations and schedule. Your written quote includes specification and supplied condition, quantity, price/currency, packaging, FOB Qingdao or FOB Lianyungang, lead time, T/T or LC payment terms and validity. Shipments use Lianyungang or Qingdao. Share the finish or pressing process you are planning, and we will help turn its material and preparation needs into a clear Sanded MDF order.
Applications
Order slab fronts, routed doors and shaker-style MDF components from our Shuyang factory. Choose raw blanks, prepared fronts or the agreed finished construction, with profiles, hinge holes and left/right pairs matched to your door schedule.
Explore applicationSheets and drawing-based components with agreed machining, face orientation, part IDs and packing groups for assembly.
Explore applicationBoards and components
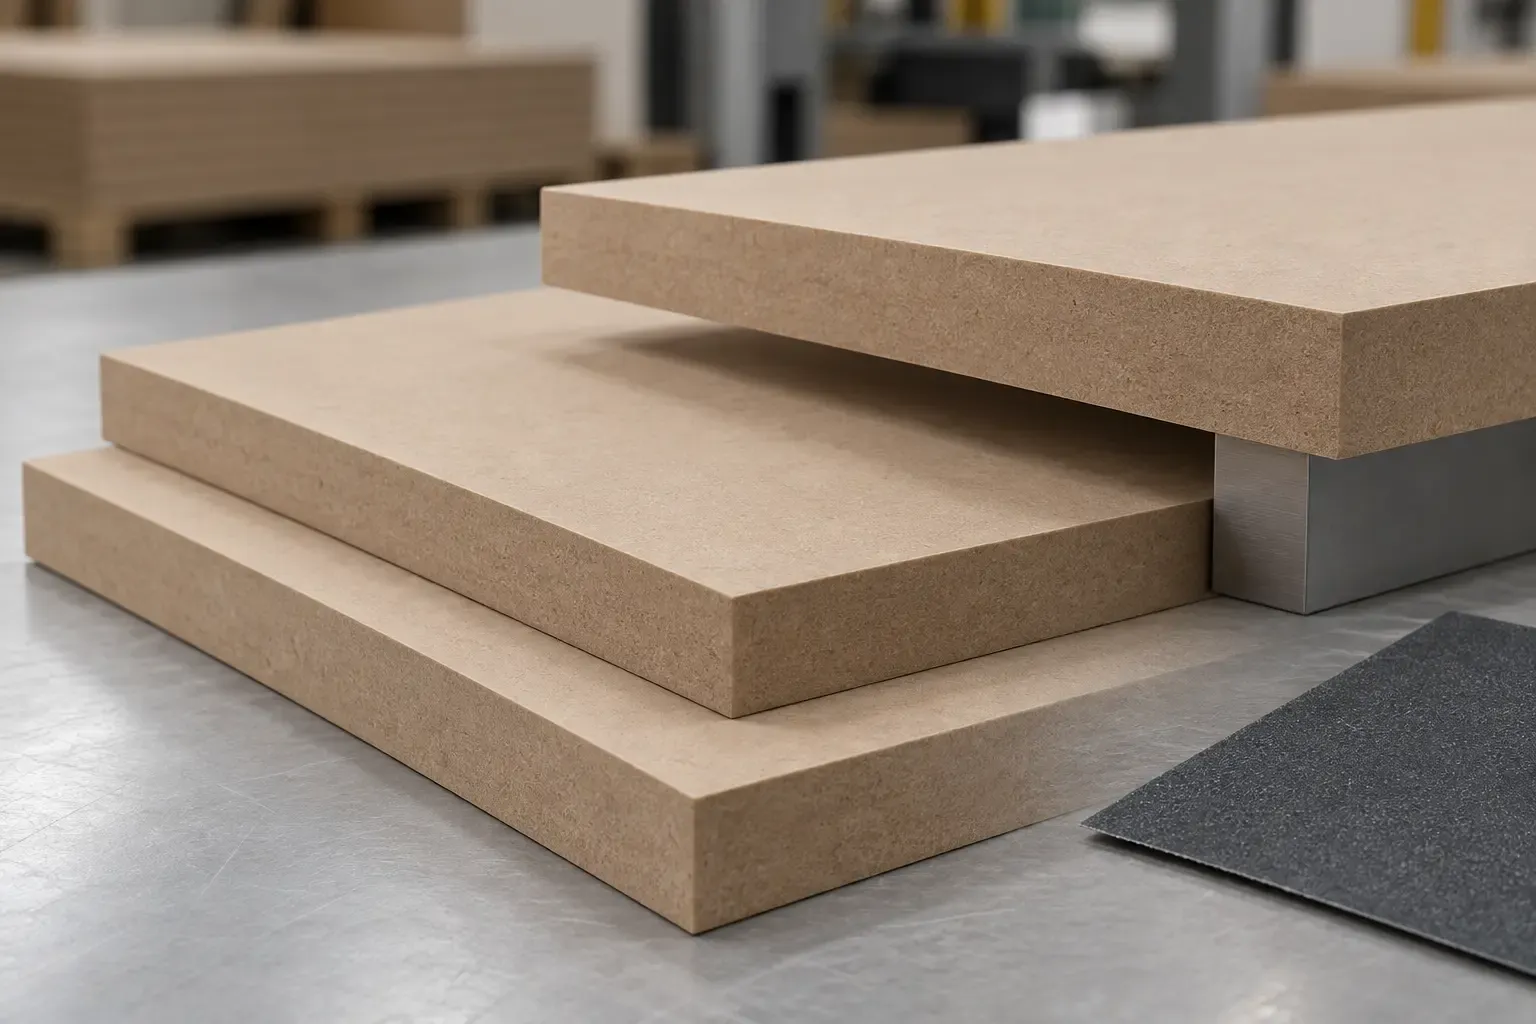
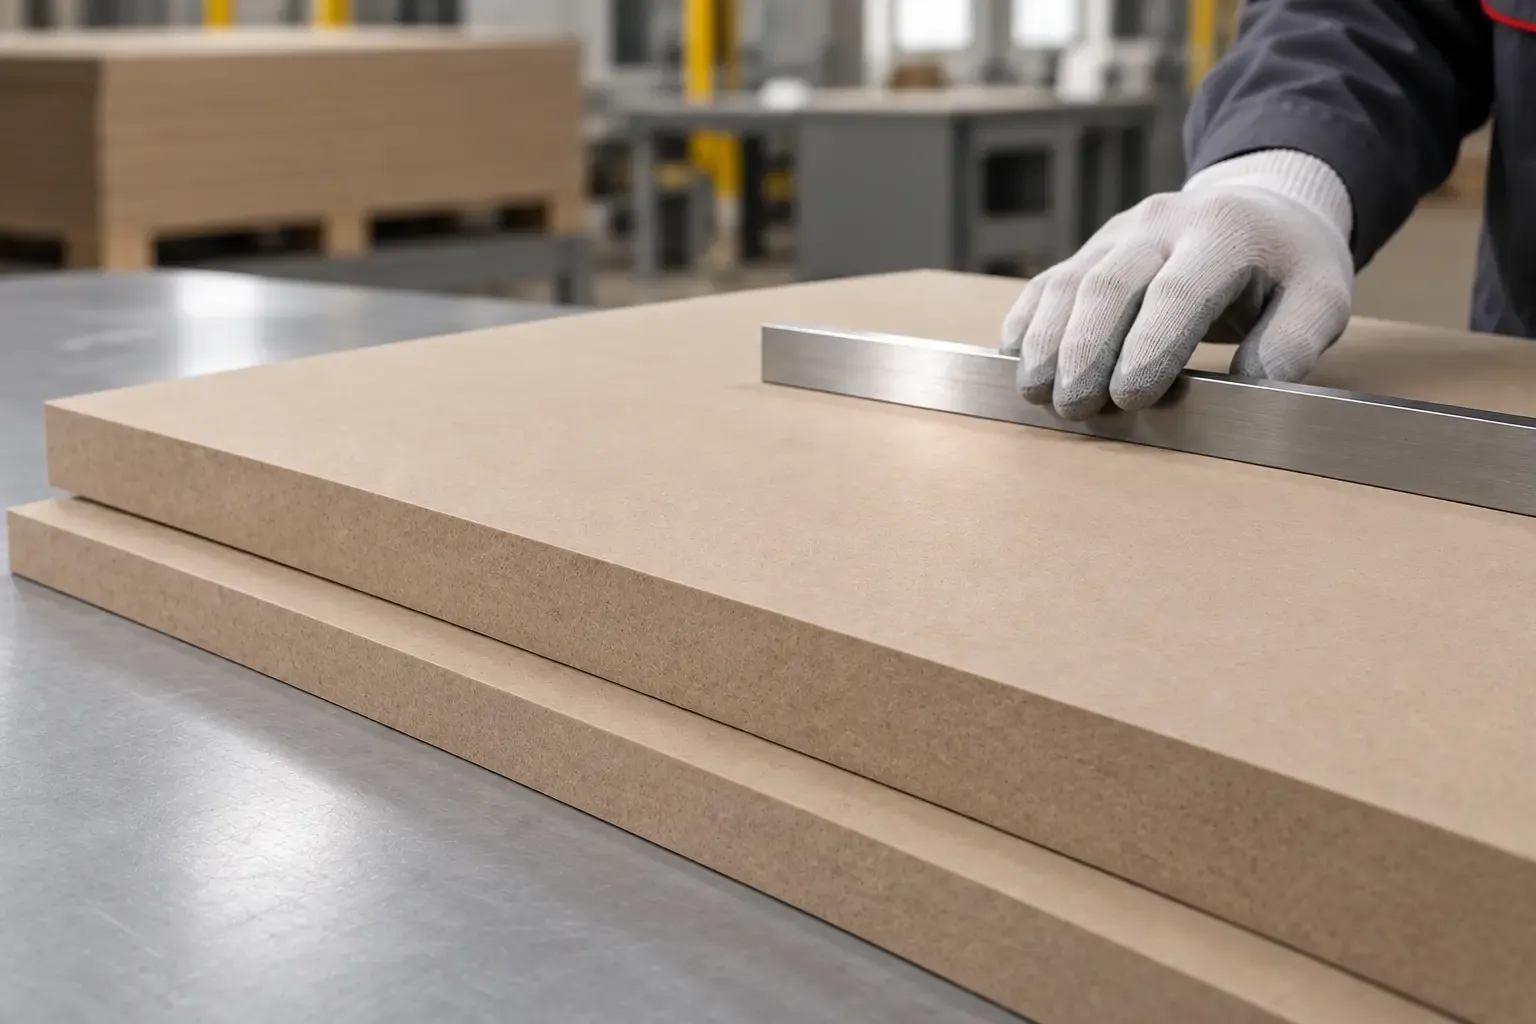
Request core and emissions information, supplied face standards and thickness checks. Record any extra preparation and the inspection method for the chosen finishing process.
Made in Shuyang, China
Work with Shuyang Cuzi MDF Co., Limited on board selection, machining, inspection and export packing. Our factory has a total daily production capacity of 500 m³ across its operations.
Made to order. The usual minimum is 1 × 20'GP per specification; mixed sizes or finishes are quoted together. Delivery lead time starts after specifications and terms are confirmed; sea transit is scheduled separately.
Freight is calculated for your ports and cargo quantity. Returns and exchanges, including timing and costs, are agreed in the order.
Delivery and freight terms · Returns and 180-day warranty · Packing and loading information
US$175–258 per m³
Your quotation confirms the specification, quantity, packaging and final price.
Buyer FAQ
Raw MDF is the general unfinished board, and our raw boards already have factory-sanded faces. Choose Sanded MDF when you need particular face preparation for pressing, veneering or painting. Any extra preparation is listed in your quote.
Sanded MDF describes the supplied factory-sanded face. Paint Grade MDF selection brings the substrate, face, cut and routed edges, primer and coating build together as one coating system. Choose around the finish you plan to apply.
A smooth factory-sanded face gives your paint process a useful starting surface. Prepare the cut and routed edges, remove dust, and choose a compatible sealer, primer and topcoat. A representative painted component establishes the preparation and appearance for the repeat batch.
State the intended downstream process, required sanding sequence or grade, acceptable marks, cleanliness, whether both faces share one standard and how the panel will be inspected.
Yes, when the selected MDF, supplied face, adhesive, pressing conditions, balancing construction and representative trial are compatible with the buyer's complete process.
Samples are free and usually in stock. You pay the courier charge, which can be credited against your order. Send the sample details and delivery address for availability, courier cost and timing. We will also give you a preparation date for custom samples.
An abrasive grade identifies the process material. Roughness describes a measured surface parameter, such as Ra or Rz, under its stated method and sampling conditions. Record the requested sanding process, actual sample, required parameter, instrument/method and allowed value for the next operation. Each record describes its own process or measured characteristic.
In the nominal example, 18.00 mm input minus 0.15 mm from Face A and 0.10 mm from Face B gives 17.75 mm prepared core. Adding illustrative permanent builds of 0.20 mm and 0.10 mm gives 18.05 mm. Actual removal, layers, bonding and dimensional tolerance follow the selected operation and measured component.
Buyer guides
The painted edge often makes the difference between a convincing MDF component and a finish that needs rework. Start with clean machining, then prepare straight edges, inside corners and profiles for the chosen coating system.
Read guideChoose MDF for painting by checking the face, cut edges and routed details with the primer and topcoat you plan to use. Raw MDF can be suitable for painting; a Paint Grade MDF order adds agreed substrate, surface and trial requirements for your painted component.
Read guideSend thickness, sizes, quantities, destination and the process you plan next. Add sanding and face criteria where you have them. We reply within 12 hours to help with a free sample and a written quote.